

UAE Food Labelling Law Requirements: What Catering & F&B Businesses Must Display
10 June 2026
Food safety compliance in the UAE extends far beyond kitchen hygiene, food handling procedures, and operational controls.
For catering companies, restaurants, bakeries, cloud kitchens, supermarkets, food manufacturers, and hospitality operators, food labelling plays a critical role in protecting consumers and ensuring regulatory compliance.
Many food businesses focus heavily on food production while overlooking one important area:
The information provided to customers on food labels.
Food labelling is not simply a packaging requirement.
It is a consumer protection requirement.
Accurate food labels help customers understand:
- Product contents.
- Allergens.
- Storage instructions.
- Product identity.
- Shelf-life information.
- Usage recommendations.
They also help businesses show professionalism, transparency, and regulatory compliance.
For growing foodservice businesses, understanding UAE food labelling law requirements is essential for avoiding compliance risks while building customer trust.
As a provider of complete commercial kitchen solutions, Al Razana Kitchen Equipment works with catering companies, restaurants, bakeries, food manufacturers, cloud kitchens, and hospitality operators across the UAE to create food production environments designed for food safety, compliance, operational efficiency, and long-term growth.
Why Food Labelling Matters in the UAE Food Industry
Food labels are often the primary source of information consumers use when making purchasing decisions.
A label helps communicate critical information about a product before consumption.
Without accurate labelling, consumers may be exposed to risks associated with:
- Food allergies.
- Dietary restrictions.
- Storage misuse.
- Product confusion.
- Incorrect food handling.
This makes food labelling a key component of modern food safety systems.
Food Labels Build Consumer Confidence.
Clear and accurate labelling supports:
- Consumer trust.
- Brand reputation.
- Transparency.
- Product credibility.
- Regulatory compliance.
Businesses that prioritize transparency often strengthen customer relationships over time.
Understanding Food Labelling Compliance in the UAE.
Food businesses operating in the UAE must ensure that food products are presented with appropriate information that allows consumers to make informed decisions.
Compliance involves much more than printing a product name on packaging.
Food labels should provide clear, accurate, and accessible information.
Who Needs to Comply?
Food labelling requirements may apply to:
- Catering companies.
- Restaurants offering packaged products.
- Cloud kitchens.
- Bakeries.
- Supermarkets.
- Food manufacturers.
- Food distributors.
- Hospitality operators.
Any business supplying packaged food products should understand applicable labelling obligations.
Why Catering Businesses Need Strong Food Labelling Systems.
Many catering companies assume food labelling only applies to retail food products.
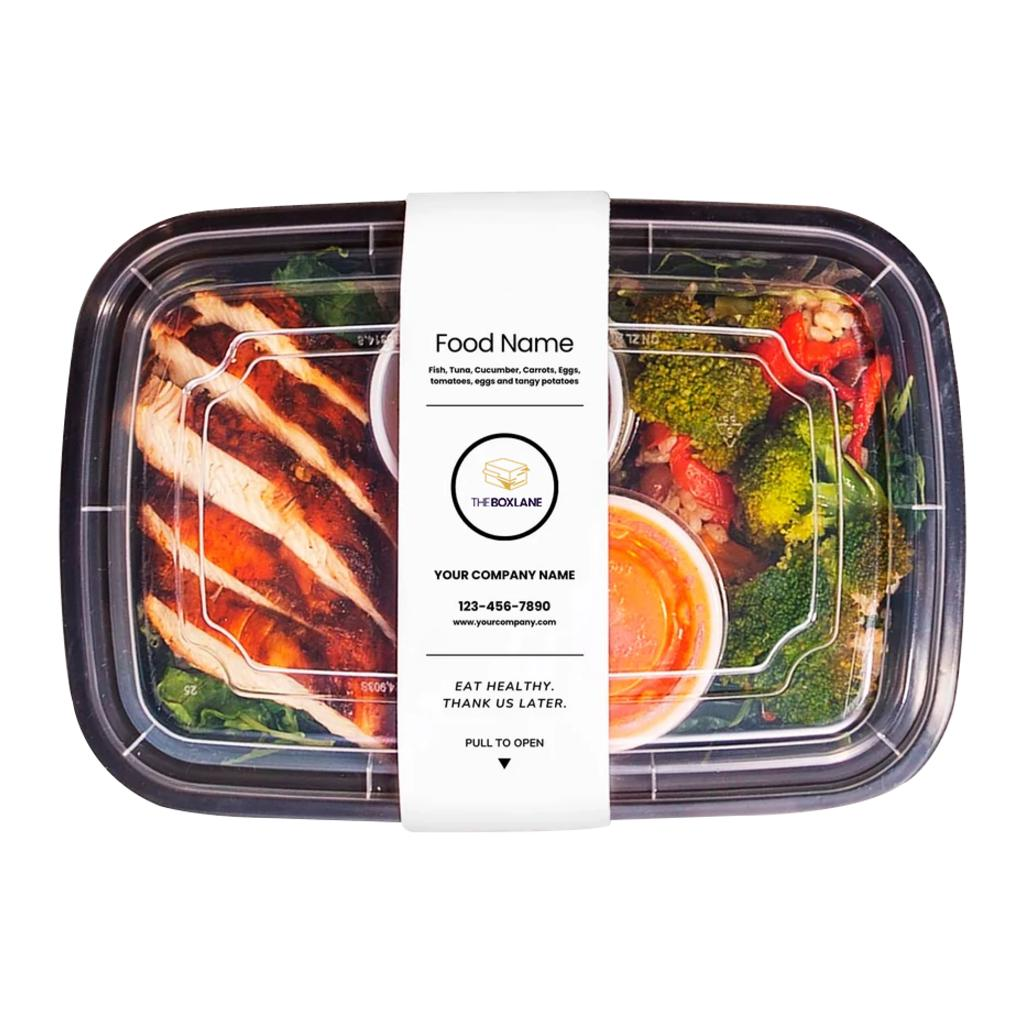
but, catering businesses often provide packaged meals, event food items, takeaway products, and corporate food services.
These situations often require accurate food information.
Catering Operations Commonly Handle.
- Corporate meal packages.
- Event food boxes.
- Grab-and-go products.
- Bakery items.
- Packaged desserts.
- Prepared meal solutions.
As catering operations expand, labelling compliance becomes increasingly important.
The Importance of Accurate Product Identification.
Consumers should be able to understand what they are purchasing.
Product identification helps eliminate confusion and supports informed decision-making.
Clear Product Identification Supports.
- Customer understanding.
- Product differentiation.
- Food safety awareness.
- Operational consistency.
Accurate naming conventions also help businesses keep organized production and inventory systems.
Allergen Declaration: One of the Most Critical Labelling Requirements.
Food allergies represent one of the most important consumer protection considerations in the food industry.
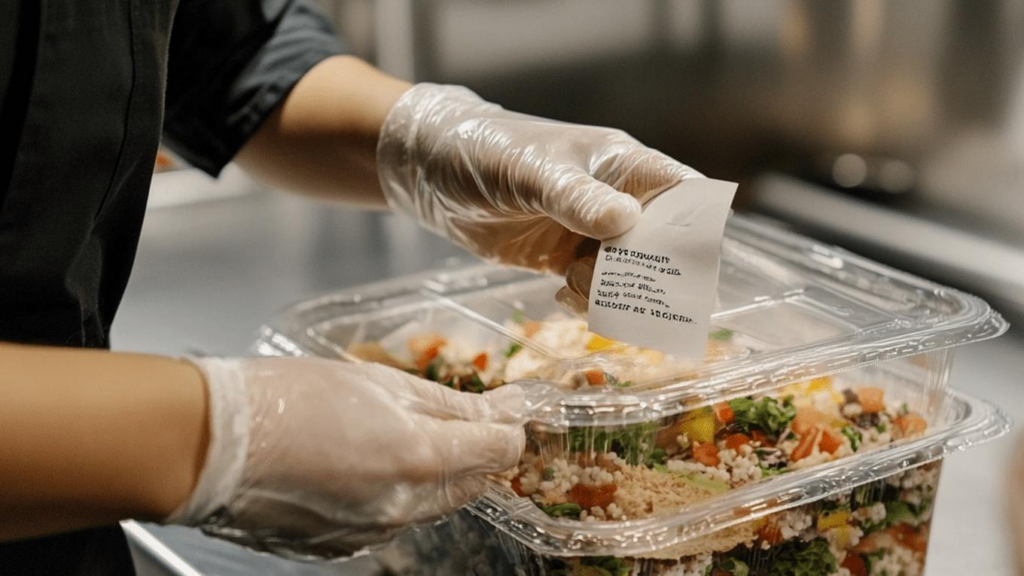
For affected individuals, accurate allergen information can be extremely important.
Why Allergen Declarations Matter.
Customers may need allergen information for:
- Health reasons.
- Dietary restrictions.
- Family safety concerns.
- Medical requirements.
Clear allergen communication helps consumers make informed choices.
Common Food Allergens.
Depending on product composition, allergen declarations may relate to ingredients such as:
- Dairy.
- Eggs.
- Nuts.
- Wheat.
- Soy.
- Fish.
- Shellfish.
Food businesses should keep strong ingredient management systems to support accurate labelling.
Arabic and English Food Labelling Considerations.
The UAE serves a highly diverse population.
As a result, multilingual communication plays an important role in consumer accessibility.
Why Dual-Language Labelling Is Important.
Providing information in both Arabic and English helps:
- Improve accessibility.
- Support consumer understanding.
- Enhance transparency.
- Improve customer confidence.
Businesses should ensure that information remains clear, accurate, and consistent across languages.
Expiry Date vs Best Before: Understanding the Difference.
One area that often creates confusion involves shelf-life information.
Consumers often encounter both expiry dates and best-before dates.
While the concepts may appear similar, they serve different purposes.
Why Shelf-Life Information Matters.
Proper date marking helps:
- Protect consumers.
- Support inventory management.
- Reduce waste.
- Improve food safety awareness.
Food businesses should establish clear internal procedures for managing shelf-life information throughout production and distribution processes.
Why Traceability Matters in Modern Food Businesses.
Food traceability has become increasingly important across the global food industry.
Traceability systems help businesses identify and track products throughout the supply chain.
Benefits of Traceability.
Strong traceability systems support:
- Food safety management.
- Product recalls.
- Inventory control.
- Consumer protection.
- Operational accountability.
The ability to track products efficiently can significantly improve risk management capabilities.
QR Codes and Digital Food Information.
Technology continues to influence the way food information is communicated.
Many food businesses now explore digital methods for providing more product details.
Benefits of Digital Information Systems.
Digital solutions can help provide:
- Product information.
- Ingredient details.
- Nutritional content.
- Brand information.
- Consumer engagement opportunities.
As technology adoption increases, digital food information systems may play a growing role in foodservice operations.
Why Food Labelling Starts in the Production Environment.
Accurate labels depend on accurate operational processes.
Errors often originate during production rather than packaging.
Production Systems Influence.
- Ingredient accuracy.
- Batch consistency.
- Traceability.
- Documentation quality.
- Product identification.
This is why food safety and production planning should work together.
How Commercial Kitchen Design Supports Compliance.
Food labelling compliance begins with operational control.
Businesses that keep organized production environments often find compliance easier to manage.
Commercial Kitchen Design Supports.
- Ingredient management.
- Production consistency.
- Workflow efficiency.
- Documentation systems.
- Traceability procedures.
These factors contribute to stronger compliance outcomes.
Why Al Razana Starts Compliance Projects With Planning.
At Al Razana Kitchen Equipment, food safety and compliance begin long before equipment installation.
The process starts with understanding:
- Production requirements.
- Product categories.
- Workflow needs.
- Storage requirements.
- Growth objectives.
This allows businesses to create operational environments designed to support both efficiency and compliance.
The Relationship Between HACCP and Food Labelling.
Food labelling and HACCP share a common objective:
Protecting consumers.
While HACCP focuses on controlling food safety hazards, labelling ensures consumers receive the information necessary to make informed decisions.
Together, these systems strengthen food safety management.
Why Commercial Kitchen Equipment Influences Compliance.
Equipment affects much more than food production.
It also influences:
- Product consistency.
- Traceability.
- Storage management.
- Workflow efficiency.
- Food safety controls.
Professional foodservice equipment helps support structured production processes that contribute to compliance.
How Al Razana Kitchen Equipment Supports Compliance-Focused Food Businesses.
Al Razana Kitchen Equipment helps catering companies, cloud kitchens, bakeries, restaurants, supermarkets, and food manufacturers create production environments designed for operational excellence and regulatory compliance.
Commercial Kitchen Design.
Creating workflows that support food safety and consistency.
Kitchen Planning & Consultancy.
Aligning operational requirements with compliance objectives.
Commercial Equipment Supply.
Providing foodservice equipment suitable for demanding production environments.
Kitchen Equipment Installation.
Ensuring proper implementation from the start.
Stainless Steel Fabrication.
Developing hygienic custom-built solutions.
Turnkey Commercial Kitchen Projects.
Delivering complete operational environments from concept through execution.
Barcode Systems and Product Traceability.
As food businesses grow, managing products manually becomes increasingly difficult.
Barcode systems help improve accuracy, efficiency, and traceability throughout the production and distribution process.
For catering companies, bakeries, cloud kitchens, supermarkets, and food manufacturers, barcode integration can become an important operational advantage.
Why Product Traceability Matters.
Traceability helps businesses:
- Track products through production stages.
- Improve inventory accuracy.
- Support food safety management.
- Strengthen recall procedures.
- Improve operational visibility.
In highly regulated food environments, traceability is often closely linked to compliance and risk management.
Benefits of Digital Product Tracking.
Modern traceability systems can support:
- Batch identification.
- Inventory control.
- Production monitoring.
- Distribution tracking.
- Operational reporting.
These systems help businesses keep greater control as they scale operations.
Common Food Labelling Mistakes Businesses Should Avoid.
Many compliance issues result from avoidable operational mistakes.
Understanding these risks helps businesses strengthen their food safety and labelling programs.
Inconsistent Ingredient Information.
Ingredient lists should remain accurate and aligned with actual product formulations.
Changes in recipes should be reflected in labelling systems.
Poor Allergen Communication.
Allergen information should be communicated clearly and consistently.
Incomplete allergen declarations can create significant risks for consumers.
Weak Documentation Systems.
Food labelling depends on accurate operational records.
Poor documentation often increases compliance risks.
Lack of Production Controls.
Without structured production procedures, maintaining label accuracy becomes more difficult.
Failing to Review Labels Regularly.
Product information should be reviewed periodically to ensure continued accuracy.
Food Packaging Compliance Best Practices.
Packaging serves both operational and compliance purposes.
While packaging protects products physically, it also serves as a communication tool.
Effective Packaging Supports.
- Product protection.
- Food safety.
- Traceability.
- Customer confidence.
- Regulatory compliance.
Businesses should view packaging as an extension of their food safety strategy.
Building Packaging Processes Into Operations.
Successful businesses establish procedures that support:
- Label accuracy.
- Consistent packaging.
- Product identification.
- Inventory management.
These practices help improve operational consistency.
Food Labelling Requirements for Catering Companies.
Catering businesses often face unique challenges when managing food information.
Unlike traditional retail products, catering operations may handle multiple menu variations, event-specific offerings, and customized food packages.
Common Catering Labelling Challenges.
These may include:
- Frequent menu changes.
- Custom meal requests.
- Event-specific packaging.
- Multiple production batches.
- Allergen management.
Structured systems help businesses manage these complexities more effectively.
Why Standardization Matters.
Standardized production and documentation processes improve:
- Consistency.
- Compliance.
- Efficiency.
- Customer communication.
This becomes increasingly important as catering businesses grow.
Food Labelling and Cloud Kitchen Operations.
Cloud kitchens continue to expand throughout the UAE hospitality sector.
Because cloud kitchens often rely on delivery and packaged food formats, food information becomes particularly important.
Cloud Kitchen Compliance Priorities.
Operators often focus on:
- Product identification.
- Ingredient management.
- Allergen communication.
- Packaging consistency.
- Traceability systems.
Strong operational controls help support customer trust and business scalability.
Managing Compliance Risk in Food Businesses.
Food labelling should be viewed as part of a broader compliance strategy.
Businesses that integrate food safety, production management, and labelling systems often achieve stronger outcomes.
Risk Management Focus Areas.
These include:
- Staff training.
- Documentation accuracy.
- Ingredient control.
- Supplier management.
- Production consistency.
- Quality assurance.
Managing these areas proactively helps reduce operational risk.
Why Commercial Kitchen Design Supports Food Labelling Accuracy.
Many business owners do not immediately connect kitchen design with food labelling compliance.
but, organized production environments often produce more accurate outcomes.
Well-Planned Kitchens Support.
- Ingredient segregation.
- Production consistency.
- Efficient workflows.
- Inventory management.
- Documentation systems.
These factors contribute directly to stronger food information management.
Design and Compliance Work Together.
The most successful food businesses integrate compliance considerations into facility planning from the beginning.
This creates more efficient and scalable operations.
Why Turnkey Commercial Kitchen Projects Help Food Businesses Scale.
As food businesses expand, operational complexity increases.
Managing separate suppliers, consultants, contractors, and equipment providers can create coordination challenges.
Turnkey project delivery simplifies this process.
Benefits of Integrated Solutions.
Turnkey commercial kitchen projects support:
- Consistent project execution.
- Better communication.
- Improved operational planning.
- Stronger workflow integration.
- Faster implementation.
These advantages become increasingly valuable for growing foodservice operations.
Why Al Razana Kitchen Equipment Is More Than an Equipment Supplier.
Food businesses require much more than kitchen equipment.
They require operational environments capable of supporting compliance, efficiency, and long-term growth.
This is where Al Razana Kitchen Equipment provides strategic value.
Commercial Kitchen Design.
Creating layouts optimized for food production and compliance.
Kitchen Planning & Consultancy.
Helping businesses align operational objectives with growth strategies.
Commercial Equipment Supply.
Providing foodservice equipment suitable for demanding hospitality environments.
Kitchen Equipment Installation.
Ensuring operational readiness from day one.
Stainless Steel Fabrication.
Developing hygienic custom-built solutions that support workflow efficiency.
Maintenance & Technical Support.
Helping businesses keep long-term operational performance.
Turnkey Commercial Kitchen Projects.
Delivering complete commercial kitchen solutions from concept through execution.
This comprehensive approach helps businesses create stronger foundations for growth and compliance.
Why Food Labelling Compliance Is a Competitive Advantage.
Many businesses view food labelling as a regulatory obligation.
but, the most successful operators understand that transparency creates trust.
Customers increasingly want information about the products they consume.
Businesses that provide accurate, accessible information often strengthen customer confidence.
Benefits Beyond Compliance.
Strong food labelling practices support:
- Brand reputation.
- Customer trust.
- Operational consistency.
- Food safety management.
- Long-term business growth.
Compliance and customer experience are often closely connected.
The Future of Food Information in the UAE.
Consumer expectations continue to evolve.
Food businesses are increasingly expected to provide greater transparency regarding ingredients, allergens, sourcing, and product information.
Technology is also changing how information is delivered.
Businesses that invest in structured systems today will be better prepared for future requirements.
Success will depend on:
- Accurate information.
- Strong documentation.
- Food safety integration.
- Traceability systems.
- Operational efficiency.
Organizations that prioritize these areas often achieve stronger long-term outcomes.
Conclusion.
Understanding UAE food labelling law requirements is essential for catering companies, restaurants, bakeries, cloud kitchens, supermarkets, food manufacturers, and hospitality operators.
Food labelling is far more than a packaging requirement.
It is a key component of food safety, customer communication, compliance, and risk management.
Accurate product information, allergen communication, traceability systems, packaging procedures, and operational controls all contribute to stronger compliance outcomes.
Businesses that integrate food labelling into their broader food safety and operational strategies are often better positioned for sustainable growth.
As a trusted provider of complete commercial kitchen solutions, Al Razana Kitchen Equipment helps foodservice and hospitality businesses across the UAE create production environments designed for compliance, efficiency, scalability, and long-term success through commercial kitchen design, planning, equipment supply, installation, fabrication, maintenance, consultancy, and turnkey project delivery.
Whether operating a catering company, cloud kitchen, restaurant, bakery, or food production facility, success begins with building the right operational foundation.
often Asked Questions.
Why are food labelling requirements important in the UAE?
Food labelling helps protect consumers by providing important information about ingredients, allergens, product identity, storage requirements, and food safety considerations.
Do catering companies need food labelling systems?
Yes. Catering companies often provide packaged meals, event food items, and takeaway products that require accurate food information management.
Why are allergen declarations important?
Allergen information helps consumers make informed decisions and supports food safety for individuals with dietary restrictions or allergies.
What is the difference between expiry dates and best-before dates?
Both help communicate shelf-life information, but they serve different purposes related to food quality and product usability.
Why is traceability important in food businesses?
Traceability supports food safety management, inventory control, product recalls, and operational accountability.
How do barcodes support food compliance?
Barcode systems improve product tracking, inventory accuracy, batch management, and operational visibility.
How does commercial kitchen design support food labelling compliance?
Organized production environments improve ingredient management, documentation accuracy, workflow efficiency, and production consistency.
What are turnkey commercial kitchen projects?
Turnkey projects include planning, design, procurement, installation, fabrication, maintenance, and project coordination under one integrated solution.
What services does Al Razana Kitchen Equipment provide?
Al Razana provides commercial kitchen design, consultancy, equipment supply, installation, stainless steel fabrication, maintenance support, and turnkey commercial kitchen solutions.
Why do food businesses choose Al Razana Kitchen Equipment?
Because Al Razana helps businesses create efficient, compliance-focused commercial kitchen environments designed for food safety, operational excellence, and sustainable growth across the UAE.


